Made in America
Get Connected With


Finding China’s top Micro Injection Mold manufacturers requires more than browsing polished factory websites. A reliable evaluation should examine mold precision, material knowledge, production controls, and communication during difficult projects. Tiny medical, electronic, and optical parts can expose weak tooling quickly. Flash, short shots, uneven cooling, or damaged ejector pins may appear after only a few cycles.
Experienced buyers should review actual workshop evidence. Look for CNC machining centers, precision grinding, electrode manufacturing, and controlled inspection areas. Ask for tolerance reports, steel certificates, mold-flow analysis, and sample parts from comparable projects. A serious supplier should explain cavity design, gate placement, venting, shrinkage, and expected mold life in clear language. ISO certification can support confidence, but it should not replace an onsite audit or independent verification.
The best manufacturer depends on your application, not advertising language. Medical components may require traceability and documented validation. Micromechanical parts may demand optical measurement and stable molding conditions. Export experience also matters, especially when drawings, packaging, and technical approvals cross borders. No ranking is perfect. Supplier capabilities change, and some impressive samples hide weak after-sales support. That is why this guide compares practical evidence, communication quality, engineering depth, and customer feedback. It aims to identify manufacturers that can build consistent Micro Injection Mold solutions, not merely attractive prototypes. A careful shortlist still needs testing. Request a detailed quotation, inspect trial parts, and confirm corrective-action procedures before placing a major order.
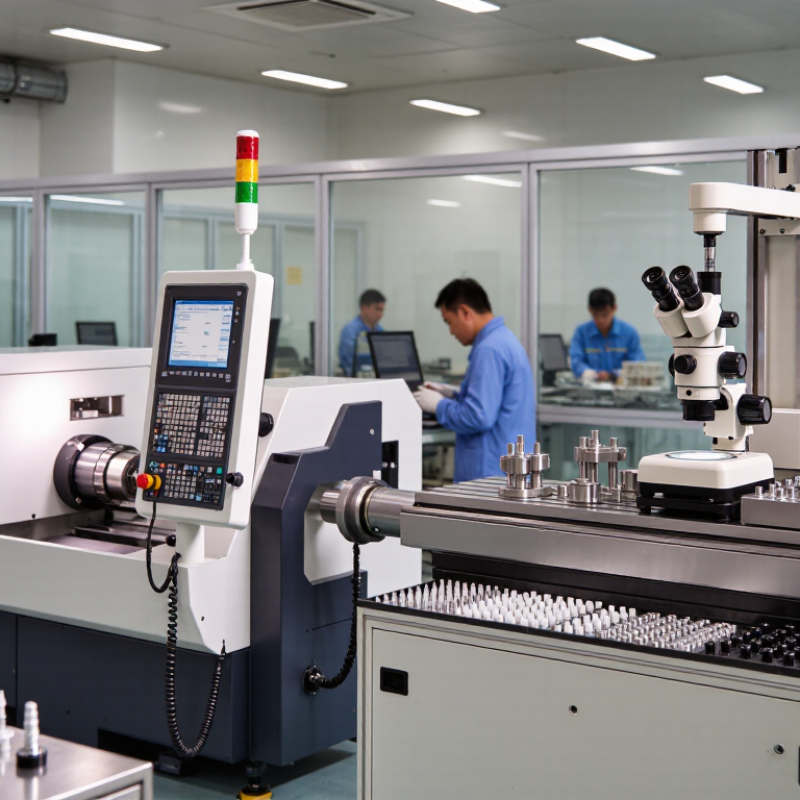
Micro injection molding produces parts with features from 0.01 to 1 mm. It is used for miniature medical, optical, electronic, and laboratory components. At this scale, a small burr can block a channel or change fluid movement. The process is not simply ordinary molding made smaller.
A capable manufacturer studies resin behavior, mold steel, gate location, and cooling balance together. A 0.01 mm rib may require polished tooling and carefully controlled filling speed.
Achieving ±0.005 mm tolerance also demands stable machines, dry material, and temperature control. Measurement should combine optical systems, microscopes, and calibrated dimensional equipment. One measurement is not enough. Process data matters.
Experienced teams also inspect the mold before production begins. They check vent depth, cavity alignment, ejector movement, and tool wear. Some materials shrink unpredictably, especially after moisture exposure. That reality can defeat an impressive drawing.
Perfect repeatability is difficult. A better approach is to validate critical dimensions through pilot runs and capability studies. Manufacturers should explain their measurement method, sampling plan, and acceptable variation clearly. They should also provide traceable inspection records, not only attractive sample parts.
Designers may need to reconsider tolerances when function allows it. Tighter is not always better. It can increase tooling time, scrap, and cost without improving performance.
China Top Micro Injection Mold Manufacturers?
China’s micro-mold industry is expanding with medical devices, micro-optics, sensors, and miniature connectors. Grand View Research estimates the global micro-molding market will maintain double-digit annual growth through 2030. Regional demand is also strengthening. China’s advanced manufacturing investment supports tighter tolerances and automated inspection.
Export data provides another useful signal. UN Comtrade records China as a major exporter under HS 8480, covering molds for plastics and rubber. However, this code does not isolate micro-injection molds. The limitation matters. Export totals include large industrial tooling, so they cannot prove a supplier’s micro-molding capability. China Customs data still shows strong international movement in tooling products, especially across electronics and medical supply chains.
Capacity should be judged beyond annual mold output. Strong manufacturers normally report cavity size, steel selection, tolerance control, mold-flow analysis, and test-shot results. A practical benchmark may include ±0.005 millimeter dimensional control, automated vision inspection, and stable production above 100,000 shots. Some factories claim higher figures, but public evidence is often thin. Ask for sample reports, maintenance records, and export documentation. A clean workshop helps, but it does not replace process data. The industry is growing quickly. Its reporting remains imperfect.
A credible ranking starts with evidence, not polished factory photos. ISO 9001 shows whether a manufacturer controls procedures, training, corrective actions, and document changes. It does not automatically prove excellent micro molds. Auditors should review current certificates, audit scope, and recent nonconformity records.
ISO 20457 deserves closer attention. It provides tolerance and acceptance guidance for plastic molded parts, but it is not a universal substitute for customer drawings. Strong manufacturers connect these requirements with mold design reviews, steel certification, cavity identification, and first-article inspection. Inspectors should examine CMM reports, microscope images, pin-gauge readings, and measurement equipment calibration. Small details matter. A 0.02 mm mismatch can affect assembly.
QC records separate capable suppliers from impressive sales claims. A useful ranking compares defect rates, sampling plans, cavity-to-cavity consistency, corrective-action speed, and traceability across production lots. Ask for redacted reports from recent micro injection projects. Check whether records include temperature, pressure, cycle time, and material batch data. Missing data is meaningful. It may indicate weak control, although busy factories sometimes document poorly rather than manufacture poorly. That distinction requires an on-site audit. I would also score communication and engineering feedback, because a technically correct mold can still fail through unclear revisions. No ranking is perfect. Evidence can become outdated quickly. Recheck certificates and QC records before approving production.
China Top Micro Injection Mold Manufacturers?
Micro injection mold performance depends on material selection, tool life, cycle time, and measurement control. For tight medical or electronic parts, hardened stainless steel often provides stable wear resistance. LCP and PEEK may require stronger tooling because they flow at higher temperatures. Softer aluminum can support early trials, but its service life is usually shorter.
Tool life is not a fixed number. Resin additives, injection pressure, cooling design, and maintenance all affect it. A well-polished cavity may reduce sticking and protect fine features. Cycle time also depends on wall thickness and cooling efficiency. A one-second reduction sounds small. Across thousands of shots, it becomes significant. Precision equipment matters here. High-speed milling, wire EDM, optical inspection, and coordinate measuring machines help control details below 0.01 millimeters. Still, equipment alone cannot correct poor mold design.
Tips: Request material certificates, dimensional inspection reports, and trial-shot data before approval. Ask how the manufacturer measures cavity wear after production testing. Check whether cooling channels reach the thickest section. A perfect cycle-time estimate is rarely possible. Real production conditions often expose small errors. Leave room for process adjustment, especially when using reinforced polymers or parts with fragile micro-features.
| Comparison Dimension | Typical Specification for Micro Injection Molds | Common Industry Range | Engineering Considerations |
|---|---|---|---|
| Mold Base Material | Pre-hardened or hardened tool steel | Approximately 30–60 HRC | Hardened tool steel offers better wear resistance and dimensional stability for long production runs. |
| Cavity and Core Inserts | Hardened steel, stainless steel, or carbide inserts | Steel for general use; carbide for highly abrasive or extremely small features | Carbide can improve wear resistance, but it requires specialized grinding, EDM, and handling processes. |
| Corrosion Resistance | Stainless tool steel for cavities exposed to moisture or corrosive polymers | Suitable for engineering plastics, medical components, and humid environments | Stainless grades reduce rust risk but may require slower machining and careful heat treatment. |
| Expected Mold Life | Production shots before major refurbishment | Prototype molds: 1,000–10,000 shots; production molds: 100,000–1,000,000+ shots | Actual life depends on steel hardness, resin abrasiveness, part geometry, maintenance, and injection pressure. |
| Typical Cycle Time | Injection, cooling, mold opening, and ejection | Approximately 5–30 seconds for small thermoplastic parts | Wall thickness, resin type, cooling-channel design, and part ejection commonly determine cycle time. |
| Micro-Feature Size | Micro ribs, slots, pins, lenses, and textured surfaces | Features from approximately 0.05–0.50 mm, depending on geometry and resin | Tool rigidity, venting, polymer flow, and demolding draft are critical at this scale. |
| Dimensional Tolerance | Cavity dimensions and molded-part control | Mold machining: commonly ±0.005–0.020 mm; molded parts vary with resin and geometry | Shrinkage, warpage, temperature variation, and process repeatability must be included in tolerance planning. |
| Surface Finish | Polished, EDM-textured, or precision-ground cavity surfaces | Approximately Ra 0.02–0.80 μm, depending on finish requirement | Optical and sealing surfaces generally require finer polishing and stricter contamination control. |
| Injection Machine Type | Electric or hybrid micro-injection molding machine | Typical clamping force: approximately 5–100 tons for small components | Stable low-shot control, accurate screw or plunger movement, and repeatable pressure are more important than size alone. |
| Machine Positioning Accuracy | Closed-loop control of injection, mold movement, and ejection | Often specified in the low-micron to tens-of-microns range, depending on the axis and machine design | Repeatability, calibration, thermal stability, and shot-size resolution affect part-to-part consistency. |
| Precision Machining Equipment | High-speed milling, wire EDM, sinker EDM, precision grinding, and laser machining | Equipment capability should support sub-0.01 mm feature control where required | A complete process chain is necessary; no single machine determines final mold precision. |
| Inspection Equipment | Coordinate measuring machine, optical comparator, vision system, and surface profiler | Measurement resolution commonly below 1–5 μm for critical micro-features | Inspection should be performed under controlled temperature and linked to documented measurement methods. |
| Common Resin Compatibility | PP, ABS, PC, POM, PA, PEEK, LCP, and medical-grade thermoplastics | Material selection depends on temperature, shrinkage, viscosity, and reinforcement content | Glass-filled and mineral-filled resins accelerate cavity, gate, and runner wear. |
| Cooling and Temperature Control | Conformal or conventionally drilled cooling channels with mold-temperature control | Mold temperature commonly ranges from approximately 20–180°C, depending on polymer | Uniform cooling reduces warpage, improves cycle stability, and supports consistent dimensions. |
| Maintenance Interval | Cleaning, lubrication, inspection, and cavity re-polishing | Basic inspection every production run; detailed service commonly every 10,000–100,000 shots | The interval should be shortened for abrasive resins, high-temperature polymers, and tight-tolerance parts. |
Note: The figures shown are typical engineering ranges for micro injection molding and are not guaranteed specifications. Final performance depends on part geometry, resin grade, mold design, process settings, machine condition, and inspection method.
China Top Micro Injection Mold Manufacturers?
Supplier selection should begin with measurable production evidence, not attractive quotations. The 2024 World Bank Logistics Performance Index evaluates six areas, including customs, infrastructure, shipment quality, and delivery timeliness. Ask each supplier for its median lead time, not its best-case promise. Record steel procurement, CNC machining, polishing, sampling, and correction time separately. A low mold price can become expensive after repeated trials.
Tolerance needs equal scrutiny. ISO 20457:2018 defines tolerance principles for injection-molded parts, but micro components often require tighter, feature-specific controls. Request a dimensional report with calibrated equipment, sampling quantity, and actual capability values. Cpk matters more than a printed tolerance claim. For example, a supplier reporting 0.02 mm variation across 30 measured cavities provides stronger evidence than a single “±0.01 mm” statement.
Validation should include mold-flow analysis, first-article inspection, capability studies, and documented process settings. The AIAG Measurement Systems Analysis reference reminds buyers that measurement error can distort capability results. Ask for gauge repeatability data. Small details decide outcomes. I would not trust perfect data without raw records; that is my practical concern. Even experienced teams sometimes accept an impressive sample before testing long-run stability. A better review checks cycle consistency, flash after extended shots, cavity balance, and dimensional drift across production lots. Industry reports discuss averages, but your mold needs evidence from its own material, geometry, and process window.
Anonymous reference profiles compare cost, lead time, dimensional tolerance capability, and validation completeness. Scores are normalized for screening: lower cost, shorter lead time, tighter tolerance, and stronger validation receive higher scores.
Typical reference values range from approximately $3,800–$8,600 per mold, 12–28 days lead time, ±0.005–±0.020 mm tolerance capability, and 65%–100% validation completeness. Confirm all figures through quotations, capability studies, inspection reports, and PPAP or equivalent validation documents.